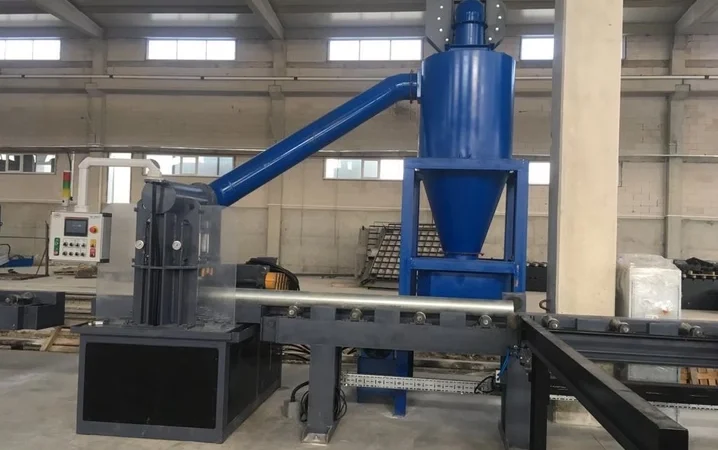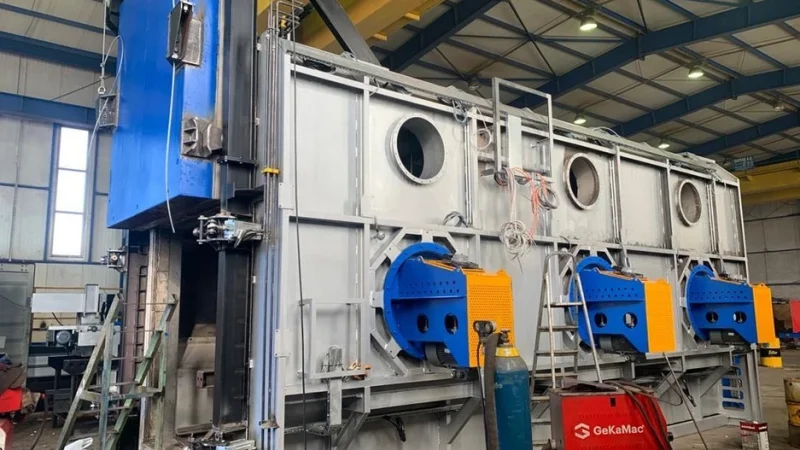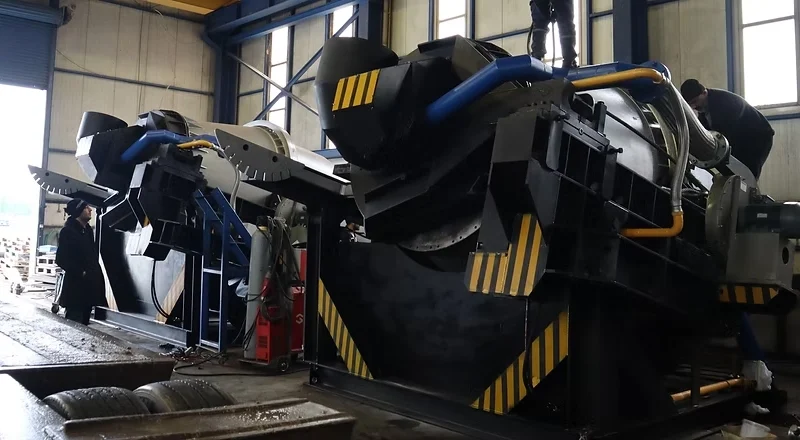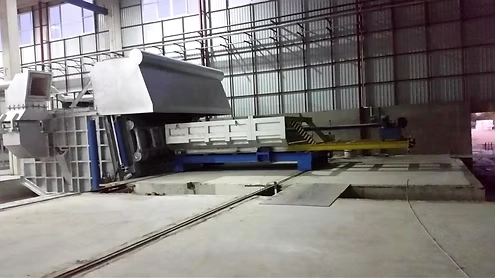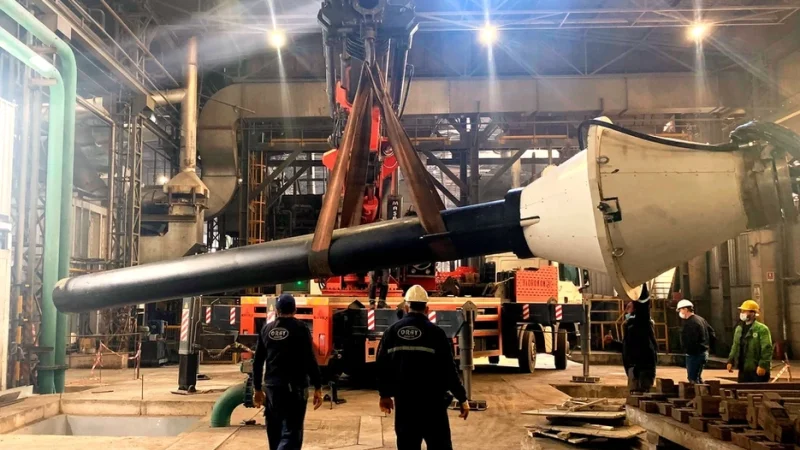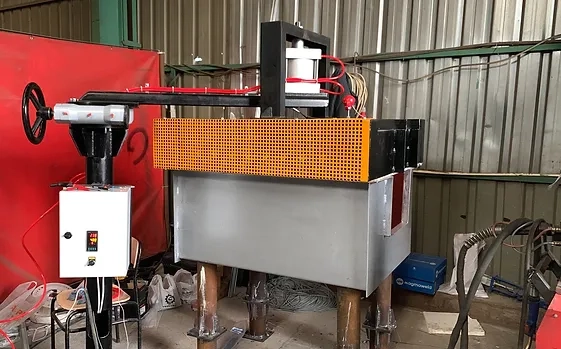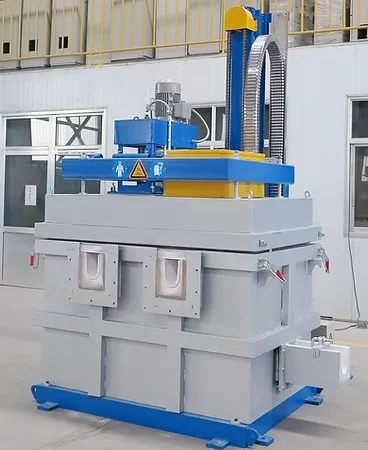
Billet Casting manufactures regenerative melting furnaces with varying capacities, tailored to specific requirements. The capacity is calculated and determined based on the casting output needs of your foundry. By utilizing a regenerative combustion system, these furnaces offer fuel savings of up to 40% compared to other types of industrial furnaces.
TECHNICAL SPECIFICATIONS FOR MELTING FURNACES
FUEL: Natural gas, 300 Nm³/hour
Inlet pressure: 300 mbar
Calorific value: Assumed to be 3,000 kcal/Nm³ ELECTRICAL: 380V, 3-phase, 50 Hz
220V, single-phase, 50 Hz
24V DC for controls
8 bar compressed air
FURNACE DATA
FURNACE TYPE: Tilting-type furnace with regenerative burners
MAXIMUM MOLTEN METAL CAPACITY: 35 tons
MAXIMUM METAL TEMPERATURE: 780 °C
AVERAGE BATH DEPTH: 650 mm
DOOR SILL LINE: 100 mm above the bath level
DOOR NO. 1
Door Operation: Hydraulic
DOOR DIMENSIONS: 1500 mm x 4750 mm
COMBUSTION SYSTEM
TOTAL BURNER CAPACITY: 5,000,000 kcal x 2 regenerative burners
Capable of melting with 2 charges per day (using 50% scrap)
Capable of melting with 3 charges per day (using 5% scrap)
BURNER IGNITION: Via spark-ignited pilot burners
FLAME MONITORING: Automatic monitoring via flame rod and flame relay
Automatic temperature control thermocouples for the bath and furnace roof
AUTOMATION AND ELECTRICAL EQUIPMENT
Brand: ABB (PLC, AC drive, circuit breaker, contactor—all equipment shall be of the ABB brand)
The electrical panel is also equipped with an air conditioning system.
DESCRIPTION OF THE REGENERATIVE BURNER SYSTEM
The furnace will be heated by a pair of regenerative hot-air burners mounted on a side wall and positioned at an angle to ensure efficient heat transfer and effective circulation of hot combustion gases within the furnace chamber.
A regenerative burner is a combustion heating system used in industrial furnaces that enables the recovery of waste heat with extremely high efficiency.
The regenerative burner system consists of a pair of burners integrated with heat reservoirs (regenerators), which fire alternately at intervals of several tens of seconds. While one burner is firing, the exhaust gas passes through the heat reservoir of the other burner, recovering energy from the exhaust stream. Subsequently, when the second burner fires, the combustion air passes through the preheated heat reservoir—recovering energy from the exhaust gas that would otherwise be wasted—thereby achieving highly efficient combustion.
Each burner will be equipped with an independent air/fuel ratio control system, regulated via valves on the fuel and air supply lines; the firing rate of the burners will likewise be controlled through these valves.
The burners will be ignited by spark-ignited pilot burners. Ultraviolet (UV) scanners will be installed on the burners to monitor the flame, and a programmed relay unit will be provided within the control panel.
Combustion air for both the main burners and the pilot burners will be supplied by separate high-pressure blowers.
Exhaust gases will be extracted by an exhaust fan. Safety controls—including fuel and air pressure switches, solenoid-operated fuel shut-off valves, a purge sequence, regulators, and fuel isolation valves—will be integrated into the combustion system.
Control Panel
All equipment required for the control and operation of the furnace is housed within a dustproof control panel. This panel should be positioned in a suitable location near the furnace.
During furnace operation, various furnace conditions and functions, as well as alarms, will be displayed on an annunciator panel located on the front of the control cabinet.
An internal automatic ignition programmer ensures that the correct ignition sequence is followed. Furnace temperature control is automatic. In the event of the furnace roof overheating, the safety control unit will shut down the burners and trigger an alarm.
The control panel will be equipped with displays and control devices for the following parameters:
- bath temperature
- roof temperature
- furnace pressure
- flame failure detection/programming units
All mains-voltage components, such as transformers and motor starters, will be housed in a separate compartment within the same panel. The panel will be fully internally wired using cable ducts and terminal blocks, and the front face will feature all necessary indicator lights, switches, and labels. The panel will undergo testing at the workshop prior to delivery. On-Site Cabling
The client shall provide all necessary mains electrical and control cabling, cable trays, junction boxes, glands, etc., between the control panels (located on or near the furnace) and all equipment supplied by ORAY (located on or adjacent to the furnace).
SCOPE OF SUPPLY
Steel structures and machined steel components. including the furnace body and structural steel, fasteners and shims, motor brackets, door, door structure, brackets, door frame and counterweight, exhaust duct, and smoke extraction hood.
Combustion system, consisting of burners, regenerative beds, heat storage media, combustion air fan, exhaust fan, pilot burner fan, switching valves, solenoid valves, control valves, flexible hoses, trim valves, isolation valves, pressure switches, flame relays, and an ignition system.
Gear motor unit for the main door, including ceramic seals, limit switches, clamping cylinders, bearings, chains, and sprockets.
Pneumatic actuator mounts and pressure sensor for the damper.
Pneumatic control, regulation, and conditioning units for the door and exhaust dampers.
Rotary-type pouring spout and connection assembly.
Float-based metal level control system for the launder.
Thermocouples for monitoring molten metal and roof temperatures.
Composite panel assembly housing the electrical control and safety system.
Refractory materials.